 Silicone Manufacturer for Custom Silicone Products
Direct answer:
Silicone molding batch size changes unit cost because machine preparation, mold changeover, material setup, process stabilization, first-article inspection, and production administration must be completed for each production release. These activities may require similar preparation whether the factory produces 300, 1,000, or 5,000 pieces.
A larger batch spreads the fixed setup cost across more accepted parts and can improve production continuity. However, unit cost does not decrease indefinitely. Silicone material consumption, molding cycle time, cavity quantity, demolding, trimming, scrap, inspection, packaging, and production capacity continue to affect the final price.
When buyers request quotations for custom silicone parts, they often compare prices at 300, 1,000, and 5,000 pieces and wonder why the unit price changes even though the material, dimensions, mold, and finished product are identical.
The answer is not simply that large orders receive better discounts. The real explanation comes from the economics of a silicone molding production batch.
Before the first acceptable part is manufactured, the factory may need to schedule equipment, prepare the mold, confirm the compound and color, stabilize molding conditions, and approve the first production samples. The cost and time involved are then distributed across the number of accepted parts produced in that batch.
Understanding silicone batch size unit cost helps procurement managers and product engineers select economical order quantities, compare quotations more accurately, and avoid unnecessary production expenses without compromising product quality.
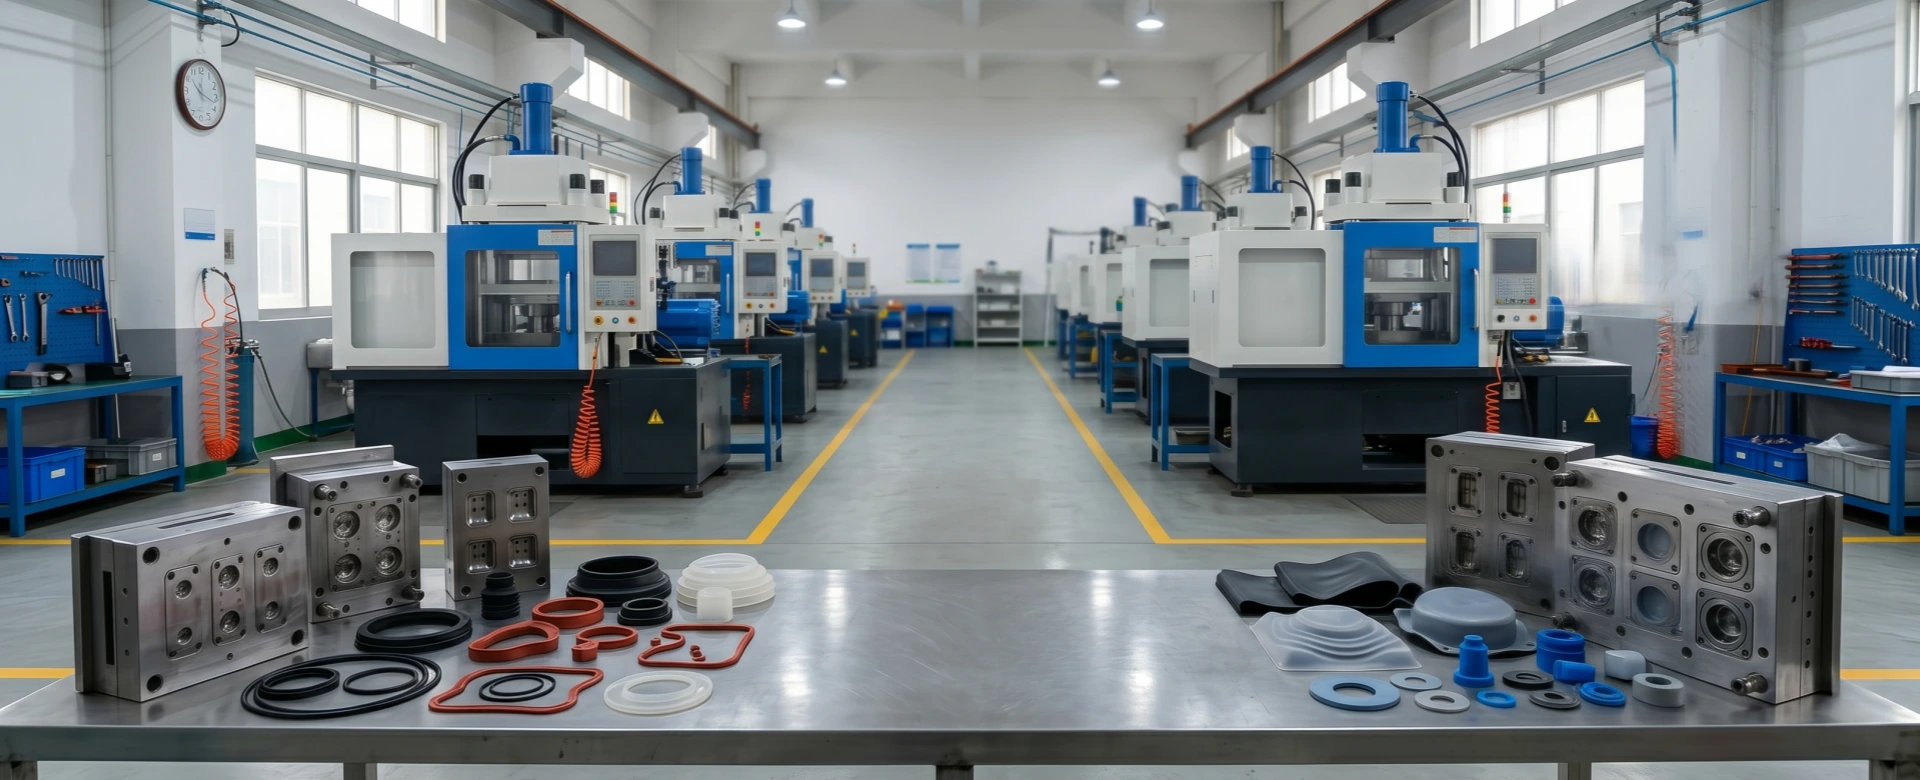
Reemane supports custom silicone compression molding, mold development, prototype sampling, and repeat production for industrial and consumer applications. We review batch quantity together with part geometry, material, tooling, cavity count, production cycle, secondary processing, and inspection requirements.
Silicone Production Cost Workflow
Production Scheduling → Mold Changeover → Material Preparation → Process Stabilization → First-Article Approval → Stable Molding → Demolding & Trimming → Inspection & Packing
What Counts as Machine Setup in Silicone Compression Molding?
Machine setup refers to the preparation required to move from an available production machine to a stable and approved manufacturing run.
It is important to distinguish this from new mold development. A custom steel mold may be a one-time project investment, while machine setup and production preparation can recur whenever a new batch is scheduled.
1. Production Scheduling and Mold Changeover
A compression molding press may already be producing another silicone component. Starting a new job can require stopping the previous run, removing the existing mold, preparing the next tool, and confirming that the machine is suitable for the new product.
The setup may involve:
- Production scheduling and machine allocation
- Retrieving the correct mold and checking its revision
- Cleaning and preparing the mold surfaces
- Installing and positioning the mold
- Checking cores, inserts, vents, and parting surfaces
- Confirming the required molding conditions
- Preparing operators and production instructions
During some of these operations, the production machine is unavailable for normal finished-part output.
This is one reason a factory cannot evaluate a very small order only by multiplying the weight of silicone by the raw-material price.
2. Silicone Material and Color Preparation
A custom silicone part may require a specific compound, Shore A hardness, cure system, color, or application requirement.
Depending on the material and processing route, the production team may need to confirm:
- Correct silicone compound and material batch
- Target hardness
- Color or Pantone reference
- Pigment preparation and uniformity
- Preform dimensions and weight
- Correct material charge for each mold cavity
- Required material documentation
A new color or compound may require additional preparation even when the same mold is being used.
3. Process Stabilization
The molding process must produce the approved part consistently. Before stable output, the team may need to confirm mold temperature, material loading, venting, curing, and demolding behavior.
This stage is particularly important when:
- The mold has been idle for a long period.
- The silicone compound has changed.
- The product uses a new color.
- The mold contains long cores or difficult undercuts.
- Critical sealing or fitting dimensions must be controlled.
- The product design has been revised.
A machine reaching its temperature setting does not automatically mean every cavity is immediately producing conforming parts.
4. First-Article Inspection
Before continuing with a production batch, the factory may check the first molded samples against the approved drawing, material specification, or reference sample.
Typical checks include:
- Critical dimensions
- Part weight where relevant
- Surface and appearance
- Flash and trimming condition
- Material and color confirmation
- Assembly fit
- Functional requirements such as sealing, grip, or retention
The required inspection depends on the project. A simple decorative product and a functional sealing component may need different approval procedures.
Buyer takeaway:
Owning the production mold does not mean every future production batch can start without setup, verification, or preparation cost.
How Fixed Setup Cost Changes the Unit Price
Manufacturing cost can be viewed as a combination of recurring batch preparation and costs that vary with the number of finished parts.
A simplified educational relationship is:
Estimated Unit Production Cost
= Direct Variable Cost per Accepted Part + Batch Setup Cost ÷ Accepted Batch Quantity
This simplified model explains why the same part can have different production costs at different batch quantities. It is not a complete commercial quotation formula: actual pricing can also include tooling, rejects, special inspection, packing, freight, overhead, risk, and commercial terms.
Example: 300 vs. 1,000 vs. 5,000 Silicone Parts
Consider a hypothetical custom silicone component manufactured using the same approved mold, compound, and process.
Assume a batch setup allowance of $120 and an additional variable production cost of $0.68 per accepted part. Assume that production efficiency and yield remain unchanged at all three quantities.
Illustrative Batch Cost Comparison
300 accepted parts
Setup allocation: $120 ÷ 300 = $0.400/part
Illustrative unit production cost: $1.080
1,000 accepted parts
Setup allocation: $120 ÷ 1,000 = $0.120/part
Illustrative unit production cost: $0.800
5,000 accepted parts
Setup allocation: $120 ÷ 5,000 = $0.024/part
Illustrative unit production cost: $0.704
These dollar figures are hypothetical examples for explaining batch cost allocation. They are not actual Reemane quotations or guaranteed prices.
The geometry, material, and mold have not changed. The reduction comes from distributing the same hypothetical setup allowance across more accepted products.
The effect is strongest when moving from a very small batch to a moderate batch. As quantity becomes larger, the setup cost represents a smaller portion of each part.
Why the Unit Price Does Not Keep Decreasing Forever
A larger batch reduces the per-piece effect of setup cost, but it does not eliminate the actual manufacturing work required for every silicone component.
Recurring costs can include:
- Silicone material consumption
- Material waste and flash
- Press operating time
- Manual loading and demolding
- Trimming and secondary processing
- Inspection
- Packaging and labeling
- Rejected parts and replacements
At a certain point, increasing order quantity may provide only a limited additional benefit unless the manufacturing process, mold cavity count, cycle time, or secondary operations can also be improved.
This explains why some price ladders show a large difference between 300 and 1,000 pieces but a smaller difference between 5,000 and 10,000 pieces.
The exact breakpoints depend on the product and production route. No universal price-discount percentage applies to every custom silicone component.
Machine Cycle Time and Cavity Count Affect Batch Economics
The number of pieces produced in each molding cycle has a direct effect on machine output.
For a simplified theoretical calculation:
Theoretical Parts per Hour
= Number of Cavities × 60 ÷ Total Molding Cycle Time in Minutes
For example, a hypothetical four-cavity mold with a six-minute complete molding cycle could produce 40 molded pieces per hour before accounting for rejects, downtime, interruptions, or downstream processing limitations.
This is only a capacity illustration. Actual silicone curing and molding cycles vary substantially according to the compound, temperature, wall thickness, mold structure, loading method, and demolding requirements.
A mold with more cavities can produce additional parts during each cycle, but the benefit must be balanced against:
- Higher mold investment
- Additional cavity loading work
- More complex material distribution
- Longer demolding time
- Press size and capacity
- Inspection and trimming output
- Expected annual demand
Learn more in Reemane’s
Silicone Compression Molding Cycle Explained
,
which covers the manufacturing stages from material preparation through inspection and packing.
Mold Cycle Time Is Not the Same as Total Batch Time
One of the most common misunderstandings in silicone production costing is using the curing timer as the complete manufacturing cycle.
A full compression molding cycle can include:
- Preform preparation and verification
- Mold opening and cleaning where necessary
- Loading material into the cavities
- Closing and venting
- Curing under the required conditions
- Opening the mold
- Demolding the products
- Preparing for the next cycle
After molding, products may still require trimming, post-curing, cleaning, printing, assembly, inspection, and packing.
A part with a short press cycle may therefore still have a relatively high unit cost if every piece requires significant manual finishing.
Conversely, a design with slightly longer curing time but easier demolding, fewer defects, and simpler trimming may achieve better overall manufacturing efficiency.
Why Scrap and Rejected Parts Matter More in Small Batches
The customer purchases accepted finished parts rather than every mold shot attempted by the factory.
If the production process generates rejected parts, the factory needs additional material, machine cycles, labor, and inspection to deliver the required quantity.
Typical molding defects can include:
- Short fill
- Excessive flash
- Trapped air or bubbles
- Tearing during demolding
- Dimensional nonconformity
- Color or surface defects
- Damage during trimming
A newly developed part may require additional process adjustments before stable output is reached. For a very small batch, the impact of these adjustments can represent a larger share of total production effort.
For this reason, a reliable quotation should consider accepted output, not simply the theoretical number of mold cycles.
Quality principle:
Reducing the curing time or removing required inspection solely to achieve a lower unit price can create costs through rejects, rework, customer complaints, and production failures.
How Color Changes and Material Changes Affect Batch Size
A purchase order for 3,000 pieces does not necessarily represent one continuous molding batch.
Consider a customer ordering:
- 1,000 black silicone covers
- 1,000 blue silicone covers
- 1,000 orange silicone covers
Although the total order quantity is 3,000 pieces, each color may require separate pigment preparation, confirmation, production records, and changeover work.
Similarly, separate production runs may be required when the customer needs:
- Different Shore A hardness levels
- Different silicone formulations
- Different mold inserts
- Several product sizes
- Different surface or logo requirements
- Different packaging or labeling configurations
The cost of changing color is not necessarily equal to a complete mold changeover. However, every additional variation should be evaluated rather than automatically treated as part of one uninterrupted production run.
Example: One 3,000-Piece Run vs. Three 1,000-Piece Runs
If a hypothetical production release carries $120 of setup cost, one continuous 3,000-piece run spreads that amount across 3,000 pieces:
$120 ÷ 3,000 = $0.040 per piece.
If production is instead scheduled as three independent 1,000-piece runs, each requiring the same hypothetical setup allowance, the combined setup amount becomes $360:
$360 ÷ 3,000 = $0.120 per piece.
This simplified illustration shows why separate releases can cost more than a continuous run. It does not mean that every actual color change, delivery split, or order restart will incur the same charge.
Should Buyers Combine Several Small Orders into One Larger Batch?
Combining production demand can sometimes reduce setup allocation and improve production continuity.
For example, a customer requiring 1,000 pieces every month may compare:
- Monthly production of 1,000 pieces
- Quarterly production of 3,000 pieces
- One larger production batch with scheduled deliveries
However, a larger production batch is not automatically the most economical overall purchasing decision.
Buyers must also evaluate:
- Inventory carrying cost
- Storage requirements
- Cash tied up in stock
- Demand uncertainty
- Risk of future product revisions
- Color or packaging changes
- Damage or deformation during storage
- Delivery schedules and warehouse capacity
A lower unit price can be outweighed by unnecessary inventory if the product is still undergoing market validation.
Purchasing recommendation:
Compare the total cost of production, inventory, delivery, and potential obsolescence rather than selecting the largest batch only because its unit price is lower.
Batch Size, MOQ, and Annual Usage Are Three Different Things
These three quantities are related, but they should not be treated as interchangeable.
Minimum Order Quantity (MOQ)
MOQ is the supplier’s practical minimum order requirement for a given product or production arrangement. It may reflect setup costs, material preparation, packaging, and other commercial factors.
Production Batch Size
Batch size is the quantity planned for a particular manufacturing run or release. It affects how setup costs, machine preparation, labor, and inspection activities are distributed across finished parts.
Annual Usage
Annual usage is the expected total number of parts required over a year. It helps evaluate mold investment, cavity count, production capacity, and long-term supply planning.
For example, a customer may have:
MOQ: 500 pieces per order
Planned batch size: 2,000 pieces
Expected annual usage: 12,000 pieces
All three numbers can be valid for the same project.
For a more detailed explanation of minimum production quantities, read Reemane’s
Custom Silicone MOQ and Factory Cost Structure
.
What Can Reduce Silicone Unit Cost Without Changing the Product?
Cost reduction should begin with production efficiency and unnecessary setup activity rather than weakening product performance.
Use Practical Batch Quantities
Request quotations at several realistic batch sizes and compare the total purchasing cost. Do not request 10,000-piece pricing if the buyer can only place and manage 300-piece orders.
Reduce Unnecessary Color Changes
Limiting the number of custom colors during the first launch can reduce pigment preparation, separate production runs, inventory complexity, and packaging variation.
Keep Approved Product Revisions Stable
Frequent changes to dimensions, hardness, texture, or logo positions may require additional sample confirmation, production adjustments, and inspection preparation.
Improve Demolding and Trimming
A suitable parting line, controlled flash, and practical demolding direction can reduce repeated manual operations throughout the production run.
Review Cavity Strategy
Where annual volume supports it, a more efficient mold cavity layout can reduce the number of molding cycles required for repeat production.
Standardize Packaging Where Possible
Common packaging materials, carton sizes, and label formats may reduce unnecessary packing changes while preserving the required brand and traceability standards.
Reemane can discuss these factors during
custom silicone mold development
and
silicone compression molding process review
.
How to Compare Silicone Quotations at Different Quantities
A useful comparison should go beyond the headline unit price.
When requesting pricing from a custom silicone manufacturer, clarify:
- Whether new mold tooling is charged separately
- Whether batch setup is included in the unit price
- Whether quantity discounts apply per SKU or across the entire order
- Whether different colors require separate production batches
- Whether the price includes trimming and secondary processing
- Whether inspection and functional testing are included
- Whether individual packaging and labels are included
- Whether the stated quantity refers to accepted finished products
- Whether future orders of a different batch size use a different unit price
- Whether the quote is EXW, FOB, or another agreed trade term
Two suppliers may quote different prices because they have included different operations or assumed different production conditions.
The lowest displayed unit price is not necessarily the lowest delivered cost for a finished and approved part.
How Reemane Reviews Batch Size and Production Cost
Reemane supports custom silicone components for sealing, protection, insulation, cushioning, grip, fit, and selected consumer product applications.
Our project review can begin from:
- STEP or STP files
- 2D engineering drawings
- Physical samples
- Product photographs and dimensions
- An existing component requiring replacement or redesign
Depending on the project, we can discuss:
- Silicone material and hardness direction
- Compression molding feasibility
- Mold design and cavity layout
- Prototype sampling
- Production setup requirements
- Practical batch quantities
- Color and material variations
- Trimming and secondary operations
- Inspection and packaging
- Repeat-order production planning
For customers with limited initial demand, our
low-volume silicone compression molding guide
explains when dedicated compression tooling is a practical manufacturing choice.
Information Needed for a Batch-Size Quotation
- STEP file, drawing, physical sample, or clear product photographs
- Product dimensions, critical tolerances, and intended function
- Silicone compound, hardness, color, and surface requirements
- Current mold status or whether a new mold is required
- Prototype or sample quantity
- Requested pricing quantities, such as 300, 1,000, and 5,000 pieces
- Expected annual usage and reorder frequency
- Number of colors, hardness grades, sizes, or SKUs
- Logo, printing, trimming, post-curing, or assembly requirements
- Functional testing, inspection, and documentation requirements
- Individual packaging, labels, and carton requirements
- Target delivery schedule and any required split shipments
Need a Custom Silicone Quote at Different Batch Quantities?
Send Reemane your drawing or sample, material requirements, expected order quantities, annual usage, color variations, and packaging needs. We will review the molding structure, tooling requirements, batch-size options, production operations, and information required for quotation.
Download the Reemane Technical Guide
Save, share, or forward the manufacturing and costing version of this article:
Silicone Batch Size, Machine Setup & Unit Cost Guide,
published by Shenzhen Reemane Silicone Technology Co., Ltd.
Frequently Asked Questions
Why is a 300-piece silicone order more expensive per part than a 3,000-piece order?
Mold changeover, machine preparation, material setup, process stabilization, and first-article inspection can be required for both quantities. In a smaller batch, these costs are spread across fewer accepted parts. The exact price difference depends on the part, mold, material, processing, and quality requirements.
Does the factory charge machine setup for every repeat silicone order?
Production preparation may recur with every batch, even when the mold is already owned by the customer. Some suppliers quote setup separately, while others incorporate it into unit pricing or minimum batch requirements. The quotation should clarify the arrangement.
Will doubling batch size cut the silicone unit price in half?
No. Only the setup-related portion becomes smaller when distributed across more accepted parts. Material, conversion, labor, inspection, secondary operations, and packaging costs remain. Doubling the batch size does not normally halve the total unit cost.
Does changing silicone color increase production setup cost?
It can. Different colors may require additional pigment preparation, cleaning, color verification, production records, and separate runs. The cost depends on the factory’s process and the exact color requirements.
Is a larger mold always better for reducing unit cost?
No. Additional cavities can increase output but also raise mold investment, loading complexity, maintenance requirements, and tool size. The appropriate cavity count depends on expected annual demand, product geometry, cycle time, and production conditions.
Can several small purchase orders be combined into one production batch?
Sometimes, when the product revision, material, color, quality requirements, and delivery schedule are compatible. Combining production can reduce repeated setup, but inventory, traceability, packing, delivery, and commercial arrangements must be agreed.
Why does the same silicone product have different unit prices across suppliers?
Suppliers may assume different cavity layouts, molding cycles, setup costs, material grades, rejection rates, trimming methods, inspection levels, and packaging requirements. Compare the complete quotation scope rather than only the displayed piece price.
What is the best batch size for a new silicone product?
There is no universal best quantity. A new product may prioritize limited inventory and market validation, while an established product may benefit from larger repeat batches. The correct quantity balances production cost, inventory risk, demand, quality, and delivery requirements.
What should I send Reemane for 300, 1,000, and 5,000-piece quotations?
Send the drawing or sample, material and hardness requirements, color, functional specifications, requested batch quantities, annual usage, number of variants, inspection requirements, packaging, and target delivery schedule. Reemane can then review the production and tooling requirements for a project-specific quotation.