 Silicone Manufacturer for Custom Silicone Products
1. The Metrological Crisis of Cavity-to-Cavity Variance
In the mass production of Liquid Silicone Rubber and High-Consistency Rubber components, scaling from a prototype mold to a high-cavitation production tool frequently introduces a severe metrological crisis: cavity-to-cavity weight and density variation. When auditing a sixty-four-cavity mold, quality control engineers often discover that components ejected from the inner cavities weigh significantly more and exhibit a higher structural density than identical components ejected from the outer perimeter cavities. In high-precision applications—such as drug delivery diaphragms or aerospace fluid seals—these microscopic volumetric fluctuations are catastrophic. A less dense component possesses inferior mechanical tensile strength and an erratic compression set profile, practically guaranteeing field failure under dynamic load.
This variance is rarely a raw material defect. It is the direct physical consequence of an unbalanced fluid delivery system. When the rheological flow of the silicone elastomer is not perfectly synchronized across the entire tooling block, the cavities that fill first undergo massive over-packing. The intense hydraulic pressure artificially compresses the polymer chains, drastically increasing the specific gravity (density) of the component. Conversely, the cavities that fill last are starved of packing pressure, resulting in underweight, porous, and mechanically weak parts. Eradicating this variance requires a fundamental rejection of primitive runner designs in favor of precision cold deck architectures.
Rheological Engineering Axiom: Geometric symmetry in a runner system does not guarantee fluidic symmetry. Variations in shear history will always dictate cavity filling, rendering geometrically balanced tools rheologically unbalanced without absolute thermal mitigation and valve synchronization.
2. The Illusion of Geometric Runner Balance and Shear Heating
The most common tooling mistake in the silicone industry is assuming that a geometrically symmetrical runner system (such as a classic “H” pattern) will deliver fluidic symmetry. In a perfectly branched runner, the physical distance from the main injection nozzle to cavity number one is mathematically identical to the distance to cavity number sixty-four. However, Liquid Silicone Rubber is a non-Newtonian, shear-thinning fluid. The elastomer flowing along the outer steel walls of the runner channel experiences intense mechanical friction, generating significant shear heating. The elastomer flowing through the dead center of the channel experiences minimal friction and remains cooler.
When this thermal gradient reaches a runner intersection, the hotter, lower-viscosity silicone splits toward the inner cavities, while the colder, higher-viscosity silicone is forced toward the outer cavities. This sheer-induced thermal imbalance destroys the uniform flow front, causing the inner cavities to fill and pack fractions of a second faster than the outer perimeter. To achieve true density equilibrium, Original Equipment Manufacturers must transition from geometrically balanced tools to rheologically balanced architectures.
3. The Absolute Necessity of Valve Gated Cold Deck Systems
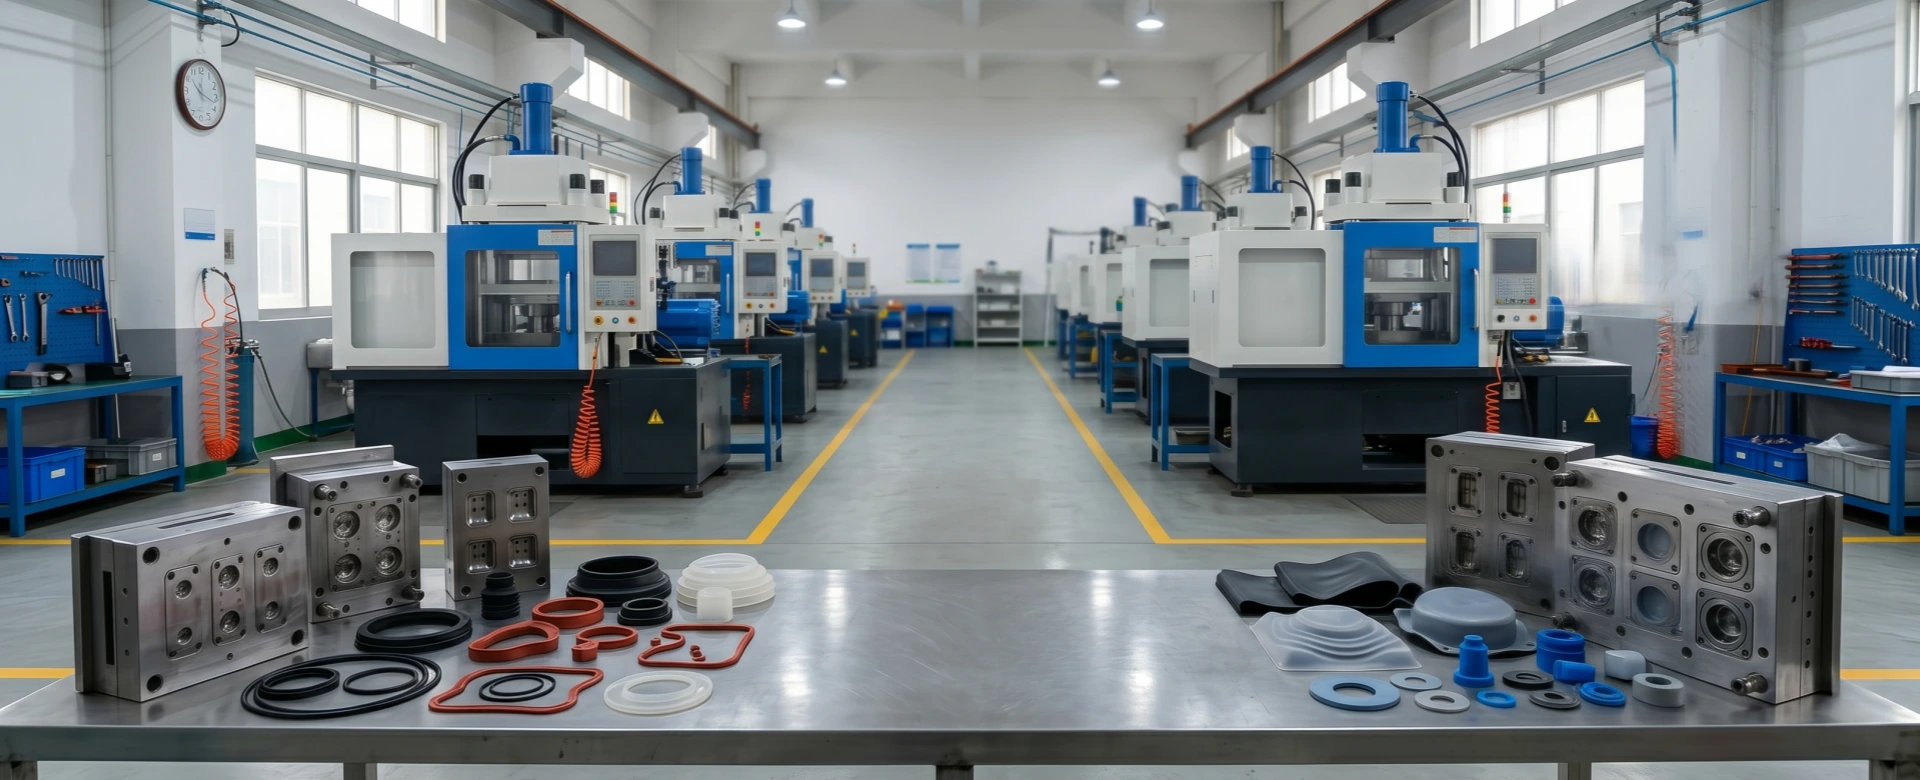
To explicitly eradicate flow imbalance and subsequent density variation, Reemane Silicone mandates the integration of advanced Valve Gated Cold Deck systems for all multi-cavity precision programs. Unlike standard open-runner systems that cure and generate massive material waste every cycle, a cold deck is a water-chilled manifold block bolted directly to the heated mold. It maintains the Liquid Silicone Rubber in a perfectly fluid, thermally stabilized state directly up to the cavity gate.
More critically, the fluid delivery is controlled by synchronized pneumatic or servo-driven valve pins. Instead of relying on fluid pressure to push the material into the cavities, the machine controller instantly retracts all sixty-four valve pins simultaneously. This guarantees that an identical volumetric shot of unvulcanized silicone is dropped into every single cavity at the exact same millisecond. By utilizing absolute mechanical synchronization rather than passive fluid dynamics, the cold deck eradicates chronological filling delays, ensuring that every cavity experiences the exact same packing pressure and yields an identical specific gravity profile.
4. Scientific Molding and Cavity Pressure Transducers
Even with a perfectly synchronized cold deck, microscopic lot-to-lot variations in the raw silicone base gum viscosity can shift the final packing density. To achieve zero-defect dimensional and weight consistency across millions of cycles, Reemane Process Engineers deploy closed-loop Scientific Injection Molding protocols. We embed highly sensitive cavity pressure transducers into the deepest, hardest-to-fill cavities of the mold block.
These sensors continuously monitor the internal fluid pressure of the silicone. The injection machine controller is programmed to transition from the velocity fill phase to the high-pressure packing phase only when the internal cavity pressure reaches a precise, mathematically verified target. This dynamic feedback loop actively compensates for any minor material viscosity shifts. If a new batch of silicone is slightly thicker, the machine automatically applies more hydraulic force to reach the target cavity pressure, guaranteeing that the density and weight of the ejected components remain mathematically identical to the approved golden sample, strictly aligning with American Society for Testing and Materials D792 auditing standards.
| Rheological Engineering Metric | Sub-Optimized Factory Sourcing | Reemane Scientific Molding Architecture |
|---|---|---|
| Runner Architecture | Geometrically balanced open runners (High variance). | Valve Gated Cold Deck (Absolute volumetric synchronization). |
| Fluid Dynamics Control | Shear-induced thermal gradients alter viscosity. | Water-chilled manifold stabilizes polymer rheology. |
| Cavity-to-Cavity Weight Variance | > 3.0% variance (Inner parts over-packed, outer starved). | < 0.5% variance across 64+ cavities. |
| Process Feedback Loop | Blind machine settings (Fails upon material lot change). | Cavity Pressure Transducers (Active density compensation). |
Eradicate Metrological Variance Before Mass Production
Do not allow unbalanced fluid dynamics and sheer heating to compromise the structural density and weight consistency of your precision components. Partner with Reemane Silicone to deploy synchronized valve gating, cavity pressure transducers, and rigorous Scientific Injection Molding protocols. To initiate a comprehensive Three-Dimensional Computer-Aided Design flow-balance audit, contact our engineering desk at sales@siliconefactories.com or inspect our Scientific Molding infrastructure at www.siliconefactories.com.