 Silicone Manufacturer for Custom Silicone Products
1. The Physics of Silicone Shrinkage and Dimensional Instability
In the high-volume procurement of Liquid Silicone Rubber and High-Consistency Rubber components, scaling a prototype from a single-cavity mold to a sixty-four-cavity production tool frequently results in catastrophic dimensional failure. Unlike rigid thermoplastics, silicone elastomers undergo a severe coefficient of thermal expansion during the vulcanization process, subsequently shrinking by two to four percent as the cross-linked polymer cools to ambient room temperature. If this shrinkage rate fluctuates between the center cavities and the perimeter cavities of a mold, the resulting batch will suffer from uncontrollable dimensional drift.
For Original Equipment Manufacturers requiring absolute adherence to International Organization for Standardization 3302-1 Class M1 tolerances, even a zero point zero five-millimeter variance can compromise the fluid-tight seal of a medical membrane or an automotive sensor gasket. At Reemane Silicone, we recognize that dimensional capability in multi-cavity tooling is not a statistical accident; it is the mathematical output of absolute thermodynamic equilibrium and rheological cavity balancing. This engineering whitepaper dissects the root causes of multi-cavity shrinkage variability and details our systemic approach to eradicating dimensional drift.
Metrology Axiom: Dimensional capability in multi-cavity tooling is not a statistical accident; it is the exact mathematical output of absolute thermodynamic equilibrium and rheological cavity balancing. You cannot inspect quality into a part that was molded under a fluctuating thermal gradient.
2. Thermodynamic Platen Equilibrium and Zonal Heating Architecture
The most profound catalyst for shrinkage variability is an inconsistent thermal gradient across the molding platen. Silicone vulcanization is a heat-driven endothermic reaction; a cavity operating at one hundred and seventy-five degrees Celsius will yield a vastly different polymer cross-link density—and therefore a different shrinkage coefficient—than a cavity operating at one hundred and seventy degrees Celsius. Standard commercial molds typically utilize primitive, single-loop heating systems, causing the core of the mold block to run significantly hotter than the outer perimeters, which lose heat to ambient factory air.
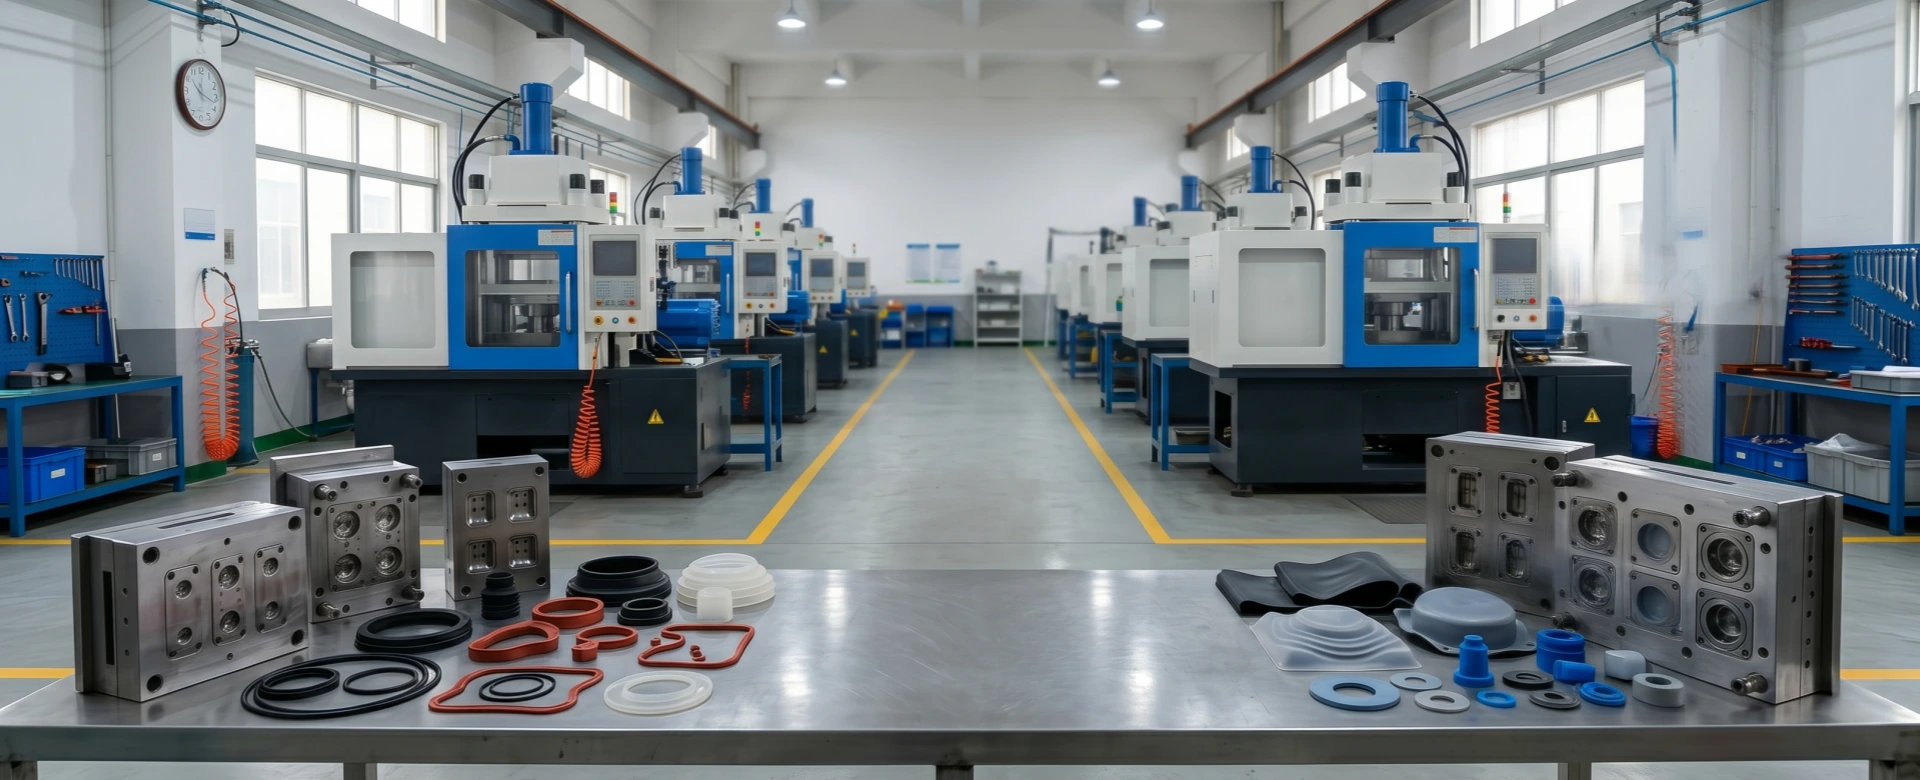
To eliminate this thermal disparity, Reemane Silicone engineers utilize advanced multi-zone Proportional-Integral-Derivative temperature controllers. We segment the tool steel into meticulously calibrated thermodynamic zones, deploying isolated cartridge heaters and independent thermocouples to continuously monitor and adjust heat input. This closed-loop thermal architecture guarantees a maximum temperature differential of less than zero point five degrees Celsius across the entire tooling block, ensuring that cavity number one and cavity number sixty-four experience identical vulcanization kinetics and identical volumetric shrinkage.
3. Rheological Cavity Balancing via Precision Cold Deck Systems
Beyond thermodynamics, fluid dynamics dictate dimensional stability. In an unbalanced tooling runner system, the low-viscosity Liquid Silicone Rubber will reach the cavities closest to the injection nozzle fractions of a second before reaching the outer extremities. This chronological delay causes the inner cavities to become heavily over-packed with material, drastically increasing their internal cavity pressure. When the mold opens, the highly pressurized inner parts will expand and shrink differently than the under-packed outer parts, generating a wide bell curve in the metrology data.
We eradicate this variable by engineering mathematically balanced runner architectures using advanced computational fluid dynamics. For high-volume medical and automotive programs, Reemane mandates the integration of Valve Gated Cold Deck systems. These Computer Numerical Control machined manifolds keep the silicone perfectly chilled and fluid until the exact millisecond of injection, dropping a synchronized, identical volume of elastomer into every single cavity simultaneously. This ensures absolute cavity pressure equalization, effectively locking in a uniform dimensional footprint across the entire shot.
4. Material Batch Consistency and Post-Cure Stabilization
Finally, variations in the raw material base gum viscosity or the dispersion of fumed silica fillers will alter the fundamental shrinkage coefficient from batch to batch. Reemane explicitly mandates the use of ultra-high-consistency, platinum-catalyzed silicone with strict lot-to-lot specific gravity controls. Furthermore, residual internal stress generated during the high-pressure molding phase can cause the component to warp or drift dimensionally weeks after production.
To arrest this post-molding drift, all precision-grade silicone seals undergo a rigorous secondary thermal annealing phase. By subjecting the components to a four-hour post-cure cycle at two hundred degrees Celsius, we force the completion of any lingering chemical cross-links and completely relieve internal mechanical stresses. The resulting elastomeric geometry is permanently locked, rendering it dimensionally inert regardless of future environmental exposure.
| Manufacturing Variable | Generic Multi-Cavity Tooling | Reemane Thermodynamic Tooling Architecture |
|---|---|---|
| Platen Thermal Gradient | > 3.0°C differential (Causes severe shrinkage variance). | < 0.5°C differential via Proportional-Integral-Derivative loops. |
| Rheological Cavity Balancing | Unbalanced runners (Inner cavities over-pack). | Valve Gated Cold Deck (Absolute pressure equalization). |
| Dimensional Tolerance Ceiling | Struggles to maintain ISO 3302-1 Class M3. | Strict adherence to ISO 3302-1 Class M1. |
| Post-Molding Stability | High risk of delayed warping due to internal stress. | Absolute lock-in via 4-hour thermal annealing. |
Eradicate Dimensional Drift in Your High-Volume Assembly
Do not allow thermodynamic imbalance and rheological pressure drops to ruin your global production runs. Partner with Reemane Silicone to deploy closed-loop, mathematically balanced mold architectures that guarantee zero-defect dimensional repeatability across millions of cycles. To initiate a comprehensive Three-Dimensional Computer-Aided Design dimensional risk assessment, contact our metrology engineering desk at sales@siliconefactories.com or inspect our Statistical Process Control infrastructure at www.siliconefactories.com.