 Silicone Manufacturer for Custom Silicone Products
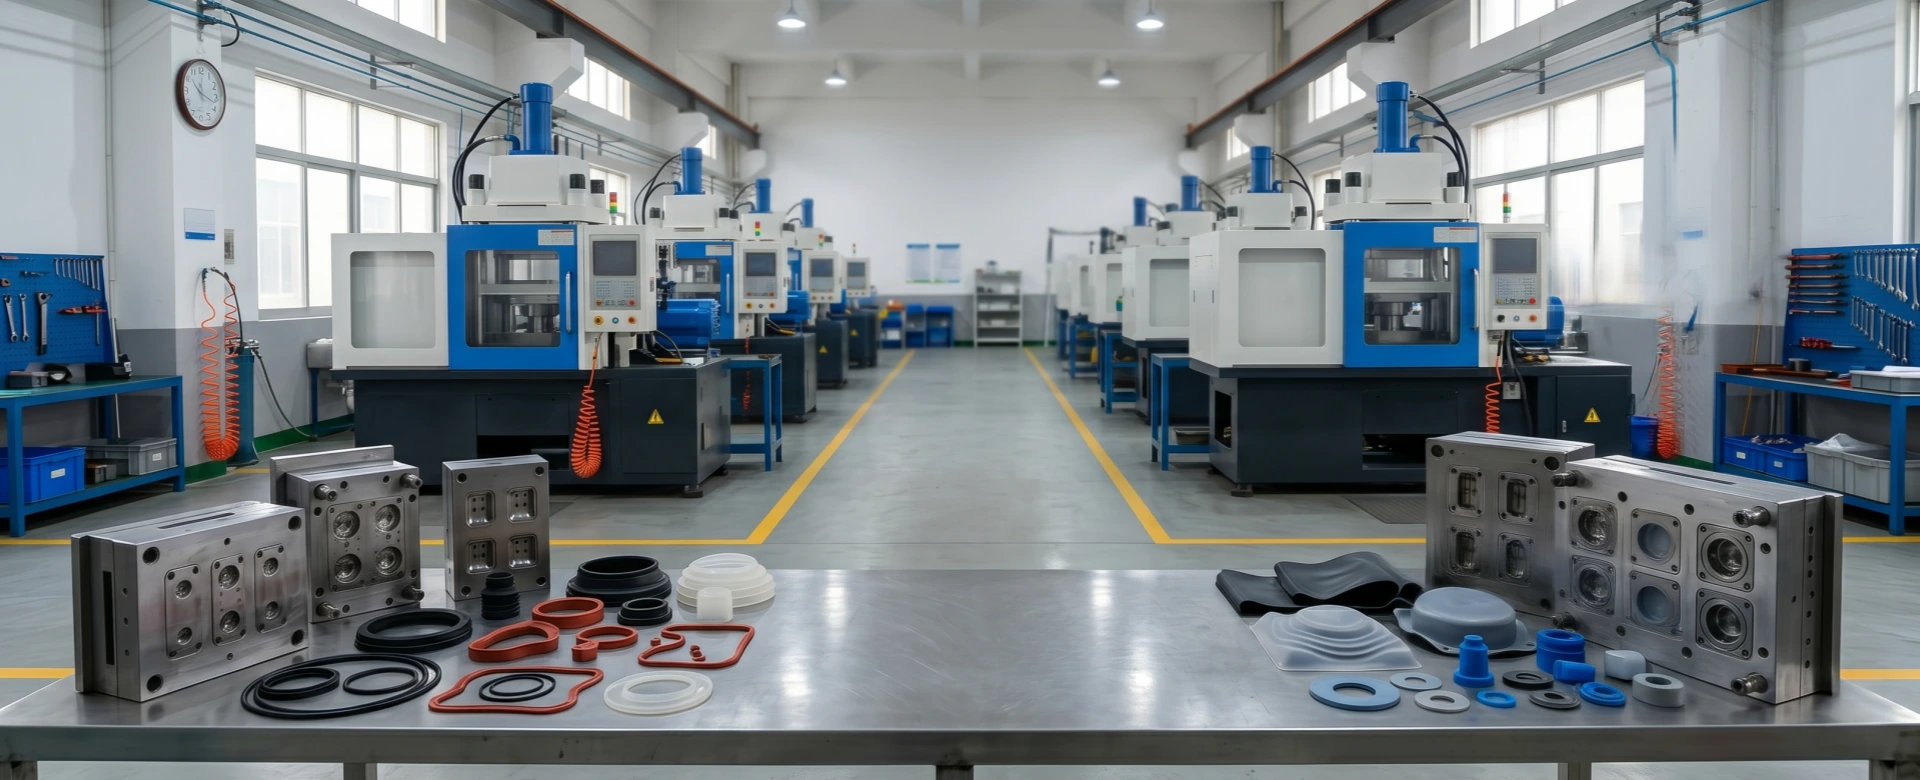
Resolving Short Shots in Silicone Molding: Advanced Mold Venting and Gate Design Strategies
In the high-precision manufacturing of Liquid Silicone Rubber components, a “short shot” is one of the most persistent and mathematically complex defects an Original Equipment Manufacturer can encounter. A short shot occurs when the unvulcanized liquid polymer freezes or is physically blocked before it can completely fill the microscopic extremities of the steel mold cavity. This results in missing geometrical features, compromised sealing lips, and instantaneous batch rejection during Quality Assurance metrology audits.
Inexperienced molding technicians instinctively attempt to solve short shots by blindly increasing the hydraulic injection pressure or extending the injection time. This primitive approach invariably causes catastrophic mold flashing, damages the delicate Computer Numerical Control milled steel, and entirely ignores the fundamental root cause. True defect resolution requires a forensic understanding of non-Newtonian fluid dynamics, meticulously engineered vacuum degassing architectures, and mathematically calculated injection gate geometries. This technical specification deconstructs the thermodynamics of silicone flow and provides the definitive engineering framework to eradicate short shots from your global supply chain.
Rheological Engineering Axiom: Liquid Silicone Rubber is a pseudoplastic fluid; its kinetic viscosity drops as shear rate increases. If you force the material through an improperly sized gate, you do not just change its speed—you fundamentally alter its thermal state, triggering premature vulcanization before the cavity is filled.
1. Atmospheric Displacement and Vacuum Venting Architectures
The most frequent physical cause of a short shot is atmospheric blockage. A high-tensile steel mold cavity is filled with ambient air. If the Liquid Silicone Rubber is injected at high velocity, the advancing flow front traps this air in the deepest blind pockets of the mold. As the air is rapidly compressed by the hydraulic injection force, it undergoes extreme adiabatic heating—often igniting and burning the leading edge of the silicone, a phenomenon known as “dieseling.”
To eliminate atmospheric blockage, elite tooling engineers deploy two critical interventions. First, micro-vents are precisely milled into the parting line of the steel mold. These vents must measure exactly between zero point zero one millimeters and zero point zero two millimeters in depth. This microscopic tolerance is large enough to allow oxygen molecules to escape, but strictly small enough to prevent the highly viscous silicone from bleeding out and causing flash. Secondly, the entire mold must be enclosed in a vacuum shroud. Before the injection valve opens, a vacuum pump extracts the ambient air, achieving a negative pressure of at least negative ninety-five kilopascals. By injecting the silicone into an absolute vacuum, atmospheric resistance is mathematically reduced to zero, allowing flawless filling of complex geometrical undercuts.
2. Shear Thinning and Gate Geometry Optimization
The gateway through which the silicone enters the mold cavity dictates the success or failure of the entire injection cycle. Because Liquid Silicone Rubber exhibits severe shear-thinning behavior, the diameter and angle of the injection gate perfectly control the viscosity of the material. If a gate is milled too large, the silicone enters the cavity too slowly and with high viscosity, losing thermal energy to the surrounding steel and solidifying before reaching the far end of the mold (a classic thermal short shot).
If the gate is milled too small, the excessive shear friction generates massive internal frictional heat. This forces the platinum-catalyzed polymer to cross-link prematurely, creating a cured rubber plug directly at the gate entrance and halting the injection entirely. Reemane engineers utilize advanced computational mold-flow software to dictate the exact gate architecture—frequently utilizing submarine gates or direct pneumatic valve gates. By calculating the exact shear rate and corresponding kinetic viscosity required to fill the specific component volume, we engineer a gate that maintains the silicone in a perfectly liquid state until the final micro-second of the filling phase.
3. Thermodynamic Balancing in Multi-Cavity Cold Runner Systems
For high-volume commercial production, Original Equipment Manufacturers require molds with thirty-two or sixty-four cavities. A severe engineering failure occurs when the cavities closest to the main injection sprue fill perfectly, while the peripheral cavities suffer from chronic short shots. This indicates a catastrophic thermal and volumetric imbalance within the cold runner distribution block.
The cold runner must maintain the Liquid Silicone Rubber at approximately twenty degrees Celsius to prevent premature curing, while the adjacent mold cavities are heated to one hundred and eighty degrees Celsius. If the thermal isolation plates separating these two zones degrade, or if the internal flow channels are not geometrically balanced to ensure perfectly equal travel distances for the fluid, the peripheral cavities will be starved of material and pressure. Reemane resolves this by employing computer-aided thermodynamic balancing, ensuring that the pressure drop and thermal exposure across all sixty-four cavities are mathematically identical, guaranteeing zero variation across the entire production lot.
4. Defect Resolution Matrix: Root Cause vs Corrective Action
| Short Shot Root Cause | Primitive / Incorrect Operator Response | Advanced Engineering Corrective Action |
|---|---|---|
| Trapped Atmospheric Air | Blindly increasing hydraulic injection pressure (Causes severe mold flashing). | Implement zero point zero one millimeter parting line micro-vents and active vacuum degassing. |
| Premature Gate Vulcanization | Lowering mold cavity temperature (Dramatically increases cycle time and lowers output). | Recalculate gate geometry to reduce frictional shear heat; verify cold runner thermal isolation. |
| Cold Runner Flow Imbalance | Manually blocking successful cavities to force material into failing cavities. | Execute complete Computer-Aided Design rheological re-balancing of the runner channels. |
| Insufficient Material Volume | Over-packing the mold, leading to dimensional bloat and weight non-conformity. | Recalibrate the injection unit dosage stroke based on exact specific gravity measurements. |
Engineer Defect-Free Production with Reemane Rheology
Eradicate short shots, eliminate atmospheric dieseling, and secure absolute dimensional conformity across multi-million part production runs. Reemane provides exhaustive computational mold-flow analysis, precision Computer Numerical Control milled vacuum venting, and fully certified International Organization for Standardization quality frameworks. To submit your component blueprint for a strict Design for Manufacturability rheological audit, contact our tooling engineering desk at sales@siliconefactories.com or inspect our advanced molding infrastructure at www.siliconefactories.com.