 Silicone Manufacturer for Custom Silicone Products
1. The Crutch of Aerosolized Mold Releases
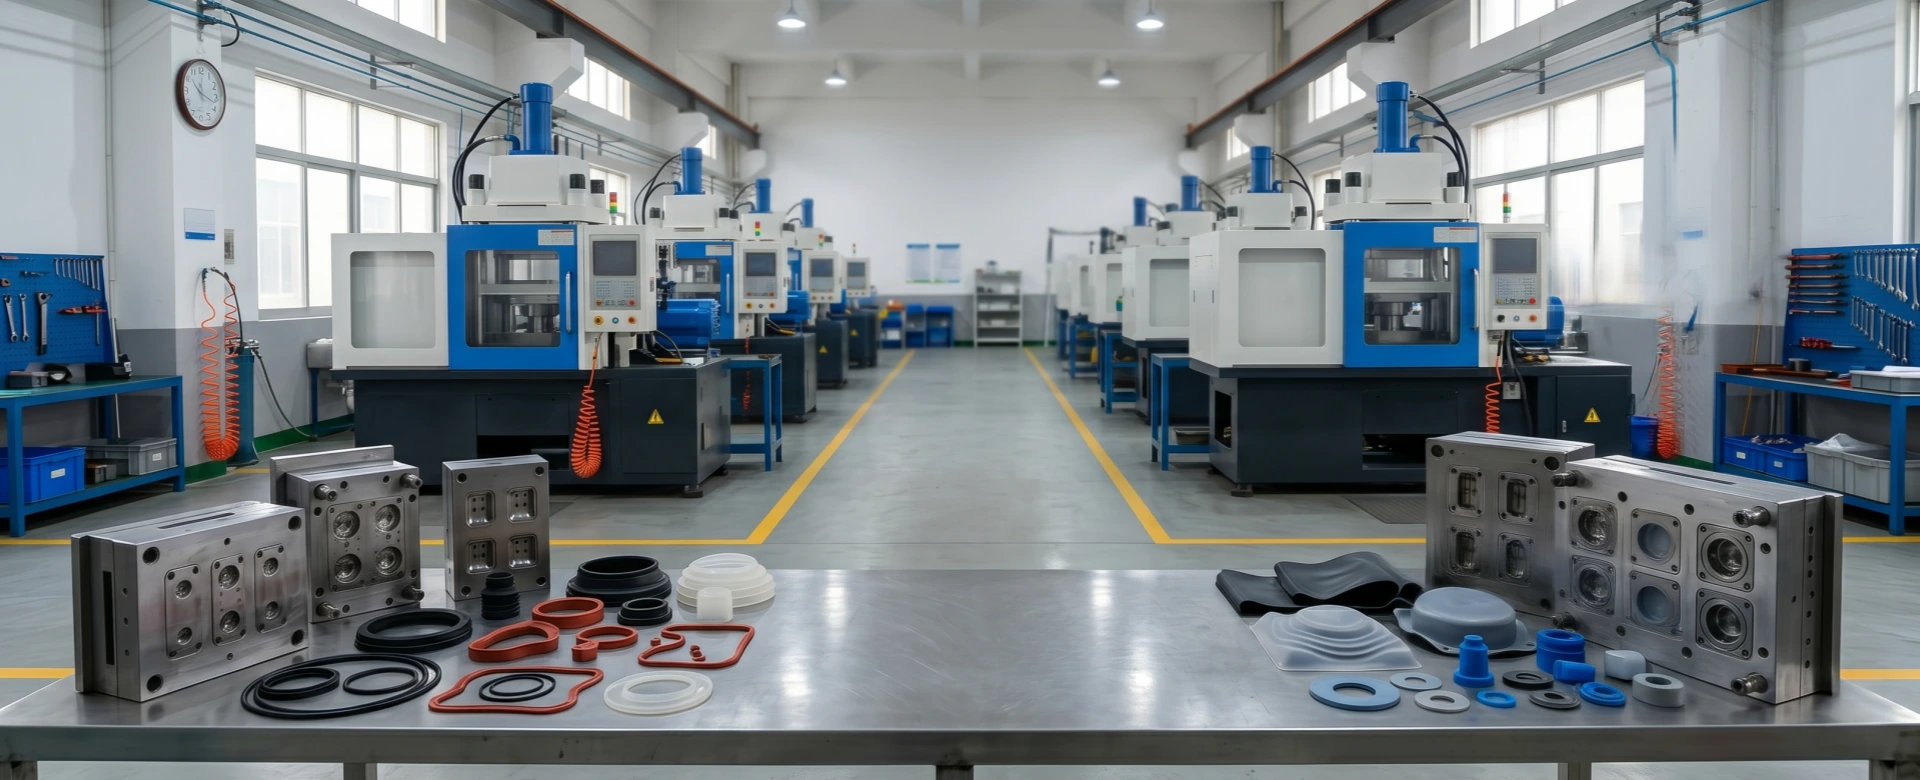
In high-volume silicone molding, extracting a complex component with aggressive undercuts or deep internal cores presents a significant mechanical challenge. When a factory’s tooling geometry is sub-optimized—lacking proper draft angles or utilizing poor surface finishes—the molded silicone will aggressively adhere to the steel cavity. To bypass these fundamental tooling flaws, novice operators frequently resort to a catastrophic crutch: flooding the hot mold with aerosolized, chemical mold release lubricants before every injection cycle.
While this allows the operator to forcefully rip the part out of the mold, it introduces severe, often irreversible chemical contamination to the silicone matrix. Silicone elastomers are highly permeable. When subjected to the extreme heat (e.g., 200 degrees Celsius) and high hydraulic pressure of the molding process, the liquid release agent does not merely sit on the surface of the part; it violently flashes into a vapor and drives itself deep into the molecular structure of the curing siloxane polymer.
Polymer Metrology Axiom: Mold release sprays are not a process enhancement; they are an admission of tooling failure. Forcing hydrocarbon solvents into a curing silicone matrix mathematically guarantees localized surface degradation.
2. Polymer Swelling and Chemical Embrittlement
The chemical composition of standard industrial demolding sprays—which often contain petroleum distillates, hydrocarbon solvents, or incompatible low-molecular-weight silicone oils—is fundamentally hostile to a cured siloxane network. When these aggressive solvents penetrate the cosmetic “A-Surface” of the component, they trigger a localized phenomenon known as solvent swelling.
As the solvent forces its way between the cross-linked polymer chains, it physically stretches and distends the molecular bonds. More destructively, petroleum-based lubricants actively extract the plasticizers and unreacted siloxanes that give the silicone its natural elasticity. When the part cools and the volatile solvents eventually evaporate, the affected surface area is left chemically denatured. The outer skin of the silicone part undergoes severe chemical embrittlement, transforming from a highly elastic rubber into a dry, crusty, and rigid layer that lacks any tensile mobility.
3. Surface Cracking Under Dynamic Load
This chemically embrittled surface acts as a profound stress concentrator. Because the outer skin of the component no longer possesses the same elongation characteristics as the untouched internal core, it cannot handle dynamic mechanical loads. When the component is subjected to flexure—either during the forceful demolding process itself, or during the very first cycle of end-user operation—the embrittled skin simply shatters.
This manifests as a network of microscopic surface cracks, commonly referred to as “crazing” or “checking.” In critical applications such as medical respiratory seals or automotive fluid diaphragms, these micro-cracks provide a direct pathway for bacterial colonization or catastrophic fluid leakage. Furthermore, in ISO 10993 biocompatibility audits, the presence of residual hydrocarbon mold release agents on a medical device guarantees an immediate and absolute failure of cytotoxicity and extractables testing.
4. Reemane’s Zero-Spray Tooling Architecture
To explicitly eradicate chemical embrittlement and guarantee absolute polymer purity, Shenzhen Reemane Silicone enforces a strict “Zero-Spray” manufacturing protocol. We refuse to compensate for poor mold design with chemical lubricants. Instead, we engineer the ejection mechanics directly into the physical tooling architecture during the Design for Manufacturability (DFM) phase.
This involves enforcing mathematically precise draft angles (minimum 1.0 degree per 25mm of depth) on all vertical cores and cavities. Furthermore, we deploy advanced surface metrology on the mold steel itself. Rather than relying on sprays, Reemane utilizes extreme SPI A2 diamond polishing combined with permanent, baked-on nano-coatings—such as Electroless Nickel PTFE (Teflon) co-deposition. This creates a permanent, frictionless tooling surface that allows even the most aggressive undercuts to demold cleanly utilizing purely mechanical air-assist ejectors, guaranteeing that the final silicone component remains 100% chemically pure, highly elastic, and completely free of embrittlement.
| Demolding Metrology Metric | Sub-Optimized Factory (Chemical Sprays) | Reemane Zero-Spray Architecture |
|---|---|---|
| Surface Chemical Integrity | Solvent penetration causes localized embrittlement. | 100% pure siloxane matrix; zero degradation. |
| Dynamic Flexure Performance | Micro-cracking (crazing) upon stretching/bending. | Infinite flexure without surface fracture. |
| Biocompatibility (ISO 10993) | Catastrophic failure due to residual hydrocarbon toxins. | Absolute compliance; zero extractable solvents. |
| Tooling Surface Treatment | Relies on aerosol lubricants to bypass poor polishing. | SPI A2 Polishing + Electroless Nickel PTFE Nano-coating. |
Eliminate Chemical Contamination in Your Tooling
Do not allow toxic mold release sprays to embrittle your cosmetic surfaces and compromise your biocompatibility standards. Partner with Shenzhen Reemane Silicone to deploy strictly engineered draft angles and permanent friction-reducing nano-coatings for flawless, purely mechanical demolding. To initiate a strict Zero-Spray DFM ejection audit, contact our engineering desk at sales@siliconefactories.com or inspect our Electroless Nano-Coating capabilities at www.siliconefactories.com.