 Silicone Manufacturer for Custom Silicone Products
1. The Rheological Challenge of Silicone Parting Line Extrusion
In the high-precision manufacturing of Liquid Silicone Rubber and High-Consistency Rubber components, unacceptable flash and burrs are universally condemned as critical quality defects. Unlike rigid thermoplastics, thermoset silicone possesses an exceptionally low rheological viscosity during the thermal vulcanization phase. It can effortlessly penetrate tooling gaps as minuscule as five micrometers (zero point zero zero five millimeters). When this low-viscosity elastomer escapes the primary mold cavity and cross-links across the parting line, it generates microscopic, razor-thin protrusions known as flash. For medical-grade seals or automotive gaskets, even a fraction of a millimeter of flash can compromise the fluid-tight integrity of the assembly, leading to catastrophic field failure.
Many generic manufacturing facilities treat flash as an inevitable byproduct, attempting to resolve the defect through post-production manual trimming or cryogenic deflashing. This reactive methodology is fundamentally flawed; manual trimming is inconsistent, introduces severe dimensional variance, and often results in micro-tearing of the silicone component itself. At Reemane Silicone, we engineer out the defect at the architectural level. This technical specification deconstructs the proactive eradication of flash, focusing on rigorous Design for Manufacturability guidelines, Computer Numerical Control machining tolerances, and the absolute maintenance of the mold parting line.
Tooling Engineering Axiom: Unacceptable flash is never a material problem; it is universally a symptom of tooling degradation or inadequate clamping force. If your factory relies on armies of manual laborers wielding trimming scissors, you are subsidizing their engineering incompetence through elevated per-unit costs and compromised dimensional integrity.
2. Architectural Design for Manufacturability and Tear-Trim Geometry
The eradication of flash begins in the Three-Dimensional Computer-Aided Design environment. The strategic placement of the parting line—the physical intersection where the two halves of the steel mold separate—is the most critical variable. Complex, multi-plane, or heavily radiused parting lines exponentially increase the risk of steel-to-steel mismatch. Reemane engineering managers enforce strict Design for Manufacturability protocols, demanding sharp, single-plane parting line geometries wherever mechanically possible.
Furthermore, by designing localized shut-off angles and utilizing strategic tear-trim grooves (often referred to as a self-deflashing mold architecture), the tooling automatically shears the residual flash during the demolding process. This engineering mechanism yields a perfect dimensional edge without requiring secondary operations, completely eliminating the human error associated with manual scissors trimming.
3. Computer Numerical Control Milling and Extreme Tooling Metallurgy
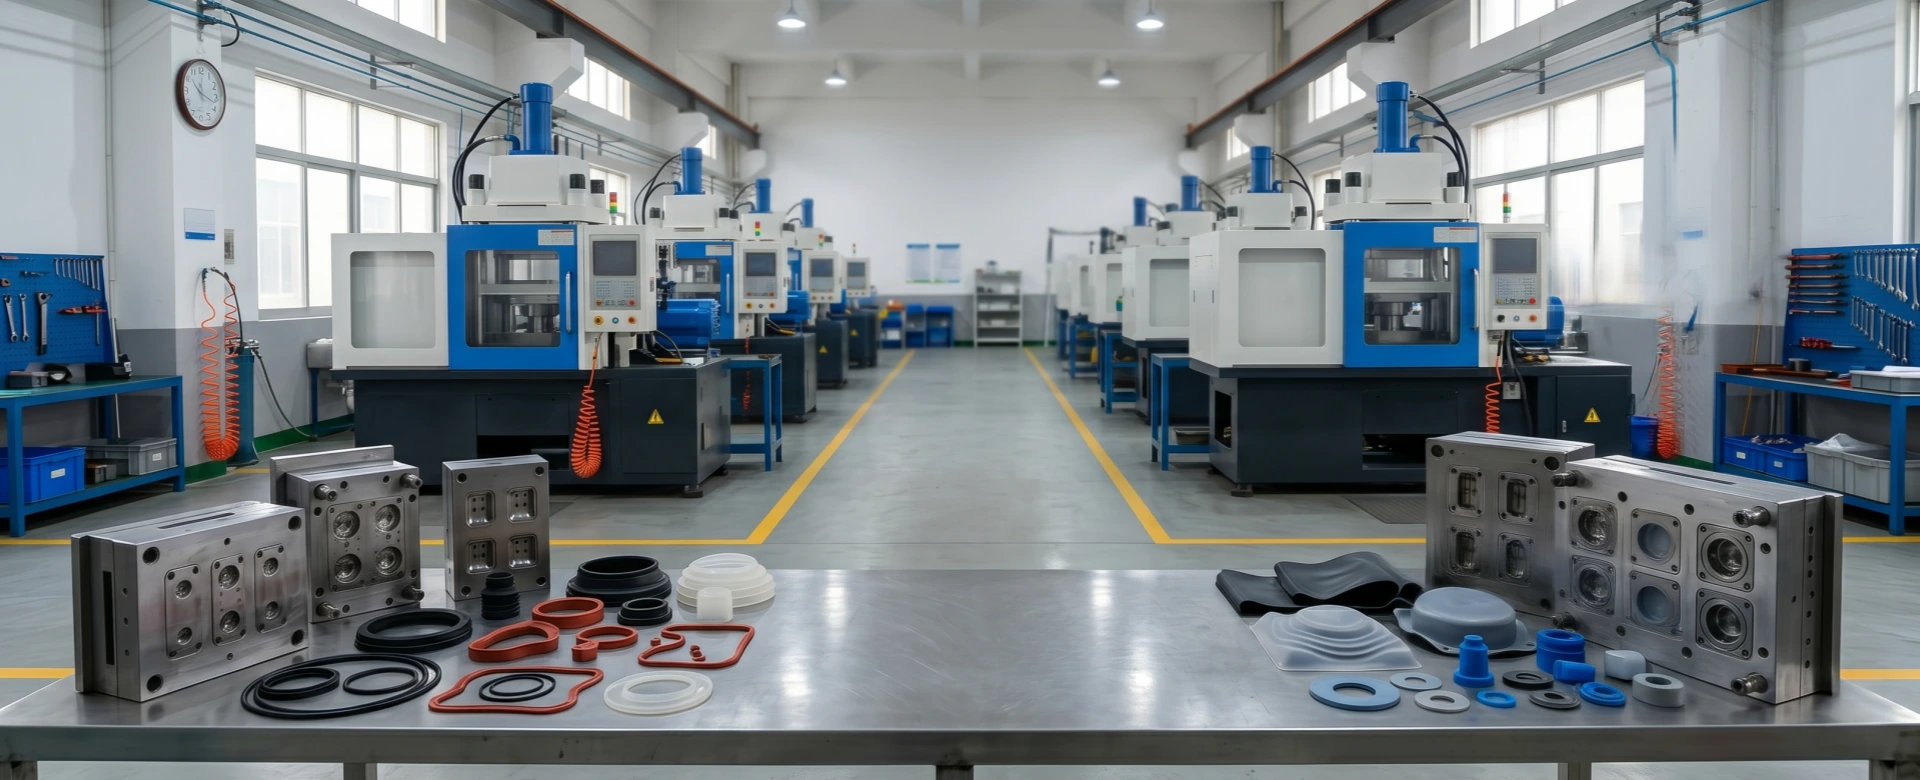
Even the most mathematically optimized geometric design will flash if the mold steel is improperly machined. Standard commercial molds are frequently cut from soft P20 steel alloys, which rapidly deform under the immense hydraulic pressure of the injection press. Reemane explicitly utilizes high-hardness S136 or H13 hardened tool steel, heat-treated to a minimum of fifty-two on the Rockwell Hardness C scale.
The mating surfaces of the parting line are subsequently subjected to extreme-precision surface grinding, ensuring a maximum flatness deviation of zero point zero one millimeters across the entire tooling block. This level of microscopic precision guarantees that when the mold closes, it creates a hermetic steel-to-steel seal that completely contains the ultra-low viscosity silicone elastomer during the high-pressure injection phase.
4. Dynamic Clamping Tonnage and Micro-Venting Systems
Flash can also be forcefully induced if the injection pressure exceeds the clamping force of the molding press. If the press cannot maintain absolute closure, the tooling will imperceptibly separate (blow open) by a few micrometers, instantly flooding the parting line with the elastomer. Reemane calculates precise hydraulic tonnage requirements based on the total projected surface area of the component cavities and the runner system, applying a massive safety factor to ensure zero tooling deflection.
Additionally, to prevent flash caused by trapped atmospheric air, we engineer microscopic vacuum venting channels. These channels are precisely sized—typically zero point zero zero three millimeters deep—to allow air to escape ahead of the flow front, while remaining completely impenetrable to the cross-linking silicone polymer molecules.
| Tooling Metric | Sub-Optimized Factory Sourcing | Reemane Precision Tooling Architecture |
|---|---|---|
| Parting Line Flatness | > 0.05mm deviation (causes severe material leakage). | < 0.01mm deviation (hermetic steel seal). |
| Mold Steel Hardness | P20 Steel (Rapid wear and cavity deformation). | S136/H13 Tool Steel (52+ HRC for infinite life). |
| Deflashing Methodology | Manual scissors trimming (high dimensional variance). | Engineered tear-trim grooves (automated, zero-variance). |
| Venting Architecture | Oversized vents causing heavy localized burrs. | 0.003mm micro-vents and vacuum assist. |
Eliminate Post-Processing Costs and Dimensional Defects
Do not subsidize manufacturing incompetence by paying for manual flash trimming. Partner with Reemane Silicone to engineer self-deflashing mold architectures built to uncompromising metallurgical standards. Ensure absolute Geometric Dimensioning and Tolerancing compliance on every batch. To initiate a comprehensive Three-Dimensional Design for Manufacturability audit, contact our engineering desk at sales@siliconefactories.com or inspect our precision tooling infrastructure at www.siliconefactories.com.